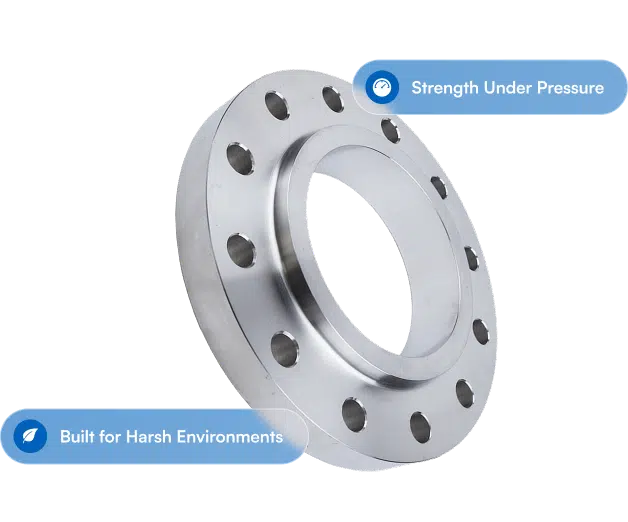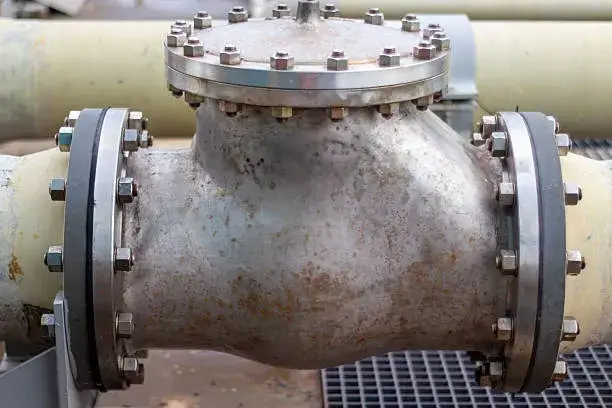
Pickin’ a flange comes down to six decisions, y’all. What’s flowin’ through the pipe, where the line lives, what the code calls for, what the budget can carry, what it’s gotta bolt up to, and what paperwork the inspector wants to see. Get dem right and the order just writes itself. Get one wrong and you’re either rebuyin’ flanges or cuttin’ out a weld dat never should’ve been made in the first place.
This here guide walks the path in the same order our sales engineers walk it when the phone rings. We been answerin’ “how do I choose a flange” since 1986, across ANSI, ASME, API, and AWWA scope, on what is by traffic the most visited flange website on the whole internet. So I reckon we got a few opinions.
If you already know your spec, head on over to our products page and grab what you need. If you need to look up dimensions, the flange dimensions and weights reference is the place. If you’re still figurin’ out which flange you actually need, y’all keep on readin’.
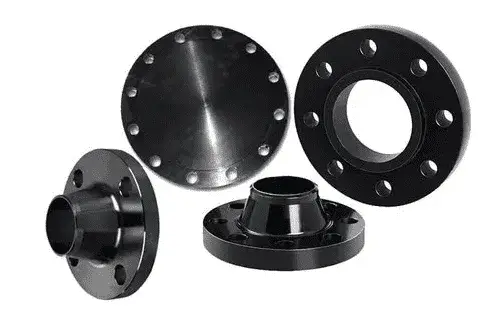
Start With What’s Flowin’ Through the Pipe
Before material, before pressure class, before face type, you gotta define the service. The fluid, the temperature, the environment, and the code or specification governin’ the project drive ever’ other decision down the chain.
Service medium. Sweet natural gas ain’t sour natural gas. Process steam ain’t utility water. Hydrocarbon liquids ain’t slurry. The medium tells you whether you’re in a corrosion fight, a temperature fight, an erosion fight, or none of the above. Common buckets: hydrocarbon (oil and gas), water and waterworks, steam and condensate, chemical process, food and beverage, slurry and abrasive service, cryogenic.
Operating environment. A flange installed indoors at ambient temperature got a mighty easier life than one buried in coastal soil, sittin’ in salt air, or settin’ on a refinery rack gettin’ splashed with whatever leaks from above. Sour service per NACE MR0175 got its own material rules. Cryogenic service got its own toughness requirements. High-temperature service got its own creep concerns.
Code or specification. This here’s the part too many buyers skip, yessir. The code drivin’ the project is what tells you which standard the flange has to meet. A few of the heavy hitters:
- ASME B31.3 for process piping
- ASME B31.4 for liquid hydrocarbon pipelines
- ASME B31.8 for gas transmission and distribution
- AWWA C207 for steel waterworks flanges
- API 6A for wellhead and Christmas tree equipment
- ASME Section VIII Div 1 for pressure vessels
- AIS and BABA requirements on federally funded infrastructure
Once you know the code, the rest of the decision tree’s already narrowed down some. ASME B31.3 in sour service rules out half the materials before you even start. AWWA C207 takes you clean off ASME B16.5 altogether. API 6A puts you in ring-joint facings whether you wanted ’em or not. The application’s the funnel, I tell you what. Everything below it is just the question of which flange falls out the bottom.
Material Selection: Match the Steel to the Service
Once you know the service, you can pick the metal. Texas Flange stocks 50+ material grades ’cause there ain’t a single right answer here. There’s a right answer for your service.
Carbon steel. ASME SA-105 forged carbon steel is the workhorse of the industry, yessir. Economical, weldable, and sittin’ in stock at any size and class. Ninety percent of the standard ANSI flange market lives right here. For low-temperature service down to -50°F, A350 LF2 is the way to go. Same machinability, better Charpy impact toughness.
Stainless grades. ASME SA-182 covers F304/304L, F316/316L, F321, and F347. F304/L handles general corrosion resistance and food and beverage cleanability. F316/L adds molybdenum for better pittin’ resistance in chloride environments, includin’ coastal service and brackish water. F321 and F347 are stabilized grades for high-temperature stainless service where intergranular corrosion’s a worry.
Chrome-moly grades. F11, F22, and F91 are the high-temperature alloys. Refinery service, power generation, steam systems above 750 degrees. F22 (2.25Cr-1Mo) is the most common in NACE sour service applications. F91 (9Cr-1Mo-V-Nb) is the modern pick for ultra-supercritical steam in power plants.
High-nickel alloys. Alloy 625, Alloy 825, Hastelloy C-276, Monel 400. Dese show up in seawater service, sulfuric acid plants, hydrofluoric acid units, and anywhere the chloride concentration eats stainless for breakfast. Lead times stretch and prices climb, but if the service demands it, ain’t nothin’ else gonna work.
Duplex and super duplex. 2205 (F51) and 2507 (F53/F55). The corrosion resistance of stainless with roughly twice the strength. Common in offshore production, chloride process, and modern sour service designs dat wanna skip carbon steel and go straight to a long-life solution.
Here’s a small material-selection cheat sheet for the common cases:
| Service | Common Material | Why |
|---|---|---|
| General process | A105 carbon steel | Economical, weldable, in stock |
| Low-temp / cryogenic | A350 LF2 | Toughness at low temperature |
| Mild corrosion | F304/L | Good general corrosion resistance |
| Chloride exposure | F316/L | Better pitting resistance |
| Sour service | F22, F51 duplex | Meets NACE MR0175 |
| High-temp / steam | F11, F22, F91 | Creep resistance |
| Seawater | Alloy 625, F55 super duplex | Resists chloride pitting |
Two material rules dat quietly cause more rebuy orders than anything else. First, mind the galvanic couple. Boltin’ a 304 stainless flange to a carbon-steel mating face in a wet environment sets up a corrosion cell dat eats the carbon steel right up. Second, weld neck flanges gotta match the run pipe metallurgy and the pipe schedule. F316 weld neck on A106 Grade B carbon pipe is a non-starter. Your WPS won’t approve it. Mighty better to know before the order ships.
If material selection runs you into corrosion territory, we got a corrosion prevention guide dat goes deeper.
Pressure Class: The Number That Has to Match the System
Pressure class is the rating system dat tells you how much pressure the flange can hold at temperature. Three numberin’ systems run the industry.
ANSI / ASME pressure classes. 150#, 300#, 600#, 900#, 1500#, 2500#. Dese are pound classes, not literal pressure ratings. A 300# flange in A105 carbon steel handles 740 psig at 100°F and 550 psig at 600°F. The pressure-temperature relationship is governed by the ASME B16.5 P-T tables for sizes 1/2″ through 24″, and ASME B16.47 for sizes 26″ through 60″. Read the tables, don’t guess, y’all.
API 6A ratings. 2,000, 3,000, 5,000, 10,000, 15,000, 20,000 psi. Dese are literal workin’ pressures for wellhead service. A 6A 5K flange means 5,000 psi workin’ pressure at the rated temperature class. Different geometry, different bore tolerances, different ring grooves. Don’t y’all cross API 6A and ASME B16.5 ratings. Dey ain’t the same flange in different uniforms.
AWWA classes. Class B, Class D, Class E, Class F. Lower-pressure waterworks service, ductile iron pipe interface, big ol’ bolt patterns. Class B per AWWA C207 is rated for 86 psi cold workin’ pressure in sizes 4″ through 24″, and 75 psi in sizes 26″ through 144″. AWWA flanges got flat faces, full-faced gaskets, and a different bolt circle than ASME B16.5 of the same nominal size. Dey ain’t interchangeable, no sir.
The pressure-temperature relationship. A flange’s rated pressure drops as the temperature rises. A 600# A105 weld neck rated for 1480 psig at 100°F is rated for 825 psig at 800°F (the upper limit for A105 in B16.5). Spec the flange to the highest pressure-temperature combination the system’s gonna see, includin’ upset conditions and hydrotest. Hydrotest is the silent killer of pressure-class decisions, I tell you what. A system designed for 1,000 psi but hydrotested at 1,500 psi needs flanges rated for 1,500 psi at the test temperature, not the design temperature.
For dimensional and pressure-temperature lookups, use the flange dimensions and weights reference. Dem tables are right there waitin’ on you.
Face Type: How the Flange Seals to the Gasket
Face type is the geometry of the sealin’ surface. Pick wrong and the gasket’s gonna leak no matter how perfect you torqued them bolts.
Raised Face (RF). The default for ASME B16.5 service. The face stands proud of the bolt circle by 1/16 inch (Class 150 and 300) or 1/4 inch (Class 400 and above per B16.5). Concentrates bolt load on the gasket, seats reliable, and works with a wide variety of gasket materials. I’d say 70 percent of ever’ flange shipped is raised face.
Flat Face (FF). Full-face gasket, no raised area. Used when boltin’ to cast-iron pumps, valves, or vessels dat would crack under the eccentric load of a raised-face flange. The rule of thumb: if the matin’ component’s brittle (cast iron, fiberglass, low-strength bronze), go flat face with a full-face gasket. If you raised-face a cast-iron pump volute, you’re gonna crack the volute. We seen it happen.
Ring Type Joint (RTJ). Metal-to-metal seal usin’ a soft iron, soft steel, or alloy ring (oval or octagonal cross section) seated in a machined groove on the flange face. Used in high-pressure / high-temperature service per ASME B16.5 600# and above, and it’s the only acceptable face type for API 6A service. Specified per ASME B16.20 for the gasket.
Tongue and Groove (TG), Male and Female (MF). Special service, yessir. The tongue or male side seats into the matchin’ groove or female side, locatin’ the gasket and keepin’ it from extrudin’. Used in lethal service, hydrogen, and certain process applications where the gasket can’t be allowed to blow out under upset conditions.
The most common face-selection mistake is wishin’ a flange was somethin’ it ain’t. The flange has to match what it bolts to. If the existin’ system’s raised face and the new component’s flat face, you don’t get to “just make it work.”
For the deeper raised-face technical breakdown, the raised-face flange guide covers the gasket math and sealin’ mechanics.
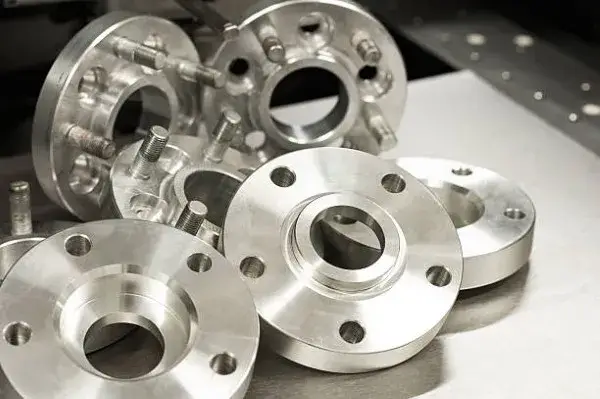
Size and Bore: Where Drawings Beat Guesses
This here’s where field surprises live. The size of a flange ain’t its outside diameter. It’s the nominal pipe size (NPS) of the pipe it bolts to. A 6-inch NPS pipe got a 6.625-inch outside diameter. Dat’s the pipe OD, not the flange OD. The flange OD is bigger ’cause it’s gotta carry bolts.
Nominal pipe size. Per ASME B36.10M (carbon steel pipe) and ASME B36.19M (stainless steel pipe), pipe sizes are nominal up to 12 inches and equal to the actual OD from 14 inches up. The bore of a weld-neck flange has to match the pipe schedule. Schedule 40, Schedule 80, Schedule XXS, and so on, all got different inside diameters. Order a 6-inch Schedule 40 weld neck thinkin’ it’ll fit your 6-inch Schedule 80 pipe and you’re gonna have a bore-mismatch problem at the welder.
Bore matching. Weld-neck flanges and socket-weld flanges got a specific bore dat matches a specific pipe schedule. Slip-on flanges, blinds, threaded flanges, and lap joints don’t care about pipe schedule ’cause dey ain’t got a butt-weld bore. If you’re orderin’ weld-necks, the schedule matters and has to be on the order. “6-inch 300# RF weld neck” is incomplete. “6-inch 300# RF weld neck Sch 40 A105” is complete.
Custom bores. If the project drawin’ calls for a non-standard bore, we can usually get it cut. Standard ANSI sizes ship from stock. Custom bores typically run two to three weeks dependin’ on grade and size.
The dimensional reference for nominal sizes, bore diameters, bolt circles, and overall lengths lives at the flange dimensions and weights page.
Standards Compliance and Mill Documentation
This here’s the paperwork section. Feels borin’ right up until the inspector asks for it and you ain’t got it.
ASME vs. ANSI naming. Most of the flange standards used to be ANSI standards. Over the last twenty-five years, ANSI handed maintenance of dem standards over to ASME. The result: B16.5 used to be ANSI B16.5, then ANSI/ASME B16.5, and is now ASME B16.5. Dey’re the same standard. The current revision is ASME B16.5-2020. ASME B16.47 (large diameter) is also at the 2020 revision. ASME B16.20 (RTJ and spiral wound gaskets) is at the 2017 revision. If a spec calls out “ANSI B16.5,” it means current ASME B16.5. Don’t get hung up on it, friend.
Buy American / AIS / BABA. Federally funded infrastructure projects (water utilities, transit, certain bridges and roads) require Build America Buy America (BABA) and AIS-compliant fittings. That means the flange has to be melted and manufactured right here in the United States, with documentation to prove it. Texas Flange stocks domestic-melt domestic-manufacture flanges across ANSI and AWWA scope. Ask before you buy. The premium ain’t huge, but the paperwork’s non-negotiable.
Material Test Reports (MTR). An MTR is the certificate from the mill showin’ the chemical composition and mechanical properties of the heat the flange was forged from. ASME SA-105, SA-350, and SA-182 all require MTRs. MTRs are available on request. Ask for it on the PO if your spec requires it. Don’t y’all go askin’ for it after the flange is welded into the line.
Certificate of Conformance (CofC). A statement from the supplier dat the product meets the specified standard. Less data than an MTR, often paired with it for AWWA and commodity-grade orders.
Mill marking. Ever’ legitimate forged steel flange got a mill stamp showin’ heat number, size, class, material grade, and manufacturer. ASME B16.5 specifies the markin’ convention (size and ratin’ on the OD, material and heat on the hub). If a flange shows up unmarked, dat’s a red flag. ASTM A961 is the general requirements specification coverin’ this for steel flanges.
For the full MTR breakdown, includin’ how to actually read one and what to look for, see the mill test report guide.
Quick Decision Flow
Six steps, in order. Walk ’em through ever’ time and the spec comes out right.
- Define the service. Medium, temperature, pressure, environment, governin’ code.
- Pick the material. Driven by the service. Carbon, stainless, chrome-moly, nickel alloy, duplex.
- Pick the pressure class. Driven by the P-T tables, includin’ hydrotest and upset conditions.
- Pick the face type. Has to match what it bolts to. RF, FF, RTJ, TG, MF.
- Pick the size and bore. NPS, schedule for weld-necks, custom bore if the drawin’ calls for it.
- Confirm standards and documentation. ASME / API / AWWA, AIS if federal, MTR if specified, CofC if required.
Step seven is unofficial and free: holler at us with what you got and we’ll fill in the blanks. Sales engineers who done spec’ed this exact line a hundred times will save you a week of diggin’ through standards on a spec you ain’t never wrote before.

Questions Folks Ask Us
What is the difference between ANSI and ASME flange standards?
Same standards, different administrators, I reckon. ANSI handed administration of the flange standards (B16.5, B16.47, B16.20, and so on) over to ASME in the last twenty-five years. A current ASME B16.5 flange is what folks still casually call an “ANSI flange.” The dimensions are the same.
How do you match a flange to a pipe schedule?
For weld-neck and socket-weld flanges, the bore’s cut to match a specific pipe schedule. Order a 6-inch 300# RF weld neck Schedule 40 to mate up to 6-inch Schedule 40 pipe. For slip-on, blind, threaded, and lap-joint flanges, the schedule ain’t part of the order ’cause the flange don’t have a butt-weld bore.
What’s the highest pressure class flange you can get?
Per ASME B16.5, the top class is 2500#. For higher pressures, you move on over to API 6A wellhead flanges, rated up to 20,000 psi. Past dat you’re in custom territory and a sales engineer oughta be on the call.
Are RF and FF flanges interchangeable?
No sir. Boltin’ a raised-face flange to a flat-face cast-iron matin’ component’s gonna crack the cast iron at bolt-up. Match the face type to the matin’ component, or use a transition spool. Raised face on raised face is fine. Flat face on flat face is fine. Mixed is a leak just waitin’ to happen.
What’s the right material for sour service?
Per NACE MR0175 / ISO 15156, sour service materials are limited to grades dat resist sulfide stress crackin’. F22 chrome-moly, F51/F55 duplex, A350 LF2 within hardness limits, and several nickel alloys all qualify. The exact grade depends on the partial pressure of H2S, the temperature, and the chloride content. Don’t y’all pick a sour-service grade off a chart. Pick it off the project’s NACE-compliant material spec.
Do I need an MTR?
If the spec calls for one, yessir. ASME B31.3 process piping, API 6A wellhead, and most government-funded infrastructure require MTRs. Texas Flange supplies MTRs on request at no extra charge for stock material.
What’s the lead time on a custom-bored flange?
Standard ANSI sizes ship from stock the same or next business day. Custom bores typically run two to three weeks dependin’ on grade and size. Special materials (high-nickel alloys, duplex) can run longer. Get the spec to us early and we’ll tell you the real lead time before you commit.
What’s the difference between a flange and a fitting?
A flange is a forged or cast disc made to bolt to a matin’ flange. A fitting (elbow, tee, reducer, cap) is a forged or fabricated piece used to change direction, branch off, or close out a pipeline. Both are pipe components, both ship from Texas Flange, both meet ASME standards. Dey just do different jobs.
Get the Right Flange the First Time
Pickin’ a flange comes down to six decisions: application, material, pressure class, face type, size and bore, standards and documentation. Walk ’em in order and the spec writes itself. Skip one and you’re rebuyin’, plain and simple.
Texas Flange been answerin’ these questions since 1986. Stock depth across ANSI, ASME, API, and AWWA standards, in 50+ material grades, with MTRs available and AIS-compliant material in stock for federal projects. Direct line to a sales engineer who’s seen the spec before.
Send us your specs and we’ll quote it right quick. If the spec’s a mess, we’ll help you clean it up before the PO ever leaves your desk.
Send us your specs | Browse stock | Look up dimensions
📞 Holler at our team today for expert guidance on your next flange order.
Last updated: May 7, 2026.
Related reading: For background on flange types, components, and how they fit into a piping system, see our complete guide to pipe flanges.