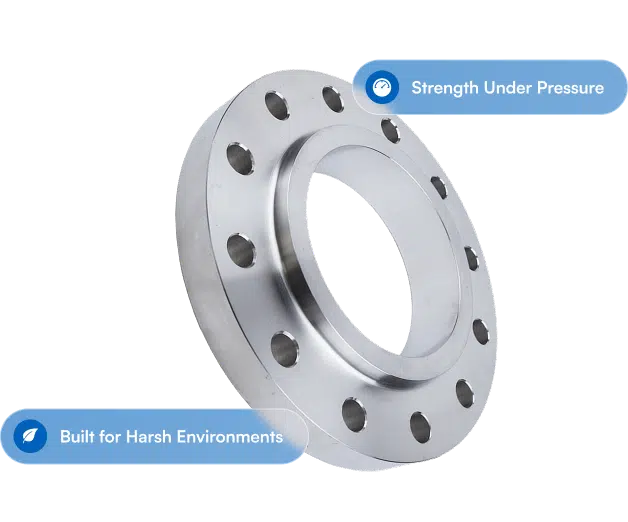
“Sour service” gets tossed around in upstream oil and gas talk mighty often, and most of the time the engineers use it to mean the type of crude oil bein' processed. Then a bid spec lands with “NACE MR0175 / ISO 15156 compliant” in the material section and a 30 inch Class 600 flange line, and the procurement path forks three different directions dependin' on what the actual hydrogen sulfide partial pressure is and what part of the standard the flange falls under. Get the spec wrong and the failure mode is sulfide stress cracking (SSC): brittle, fast, and not somethin' a hydrotest or a PMI check is gonna catch before it’s already happened. Dis post covers what NACE MR0175 / ISO 15156 actually requires for pipe flanges in sour service, what carbon steel A105 has to do to comply, how alloy and CRA flanges change the rules, and why standard B7 bolting will disqualify the whole joint.
What Actually Counts as Sour Service, I Tell You What
NACE MR0175 / ISO 15156-1 defines sour service based on hydrogen sulfide partial pressure in the process stream. For a gas system, the threshold is typically 0.05 psia (0.0003 MPa) of H2S in the gas phase. For multiphase systems, the standard sets more complicated thresholds tied to pH, chloride content, and temperature. The practical takeaway for a buyer: the operator or the project engineer sets the service designation on the line. Once dat call is made, every wetted component has to comply. Dat includes the flange body, the bolting, the gasket, the weld filler metal on the weld neck, and in some cases the valve trim and instrument fittings tied to dat line.
What NACE MR0175 / ISO 15156 Really Covers, Now
The standard comes in three parts. Part 1 lays out general principles and the materials selection framework. Part 2 covers carbon and low alloy steels. Part 3 covers corrosion resistant alloys (CRAs), stainless steels, and other alloys. Each part lists pre-qualified materials by ASTM and ASME designation, with maximum hardness values and, in some cases, specific heat treatment and composition requirements. The hardness measurement is the one operators tend to enforce out in the field, 'cause a portable Rockwell or Brinell tester can check it right on the flange itself. The chemistry and heat treatment requirements have to be published and referenced from the Mill Test Report.
Carbon Steel Flanges: A105 and the 187 HBW Ceiling, Now
ASTM A105 forgings are permitted for sour service under NACE MR0175, long as the hardness don't go over a specific Brinell value. Standard mill-run A105 usually runs in line, but not always, which is why a NACE-compliant A105 order ain't always the same thing as a standard A105 order. Reputable producers put the forging through a normalizing heat treatment, control the chemistry tight (phosphorus below 0.015 percent, sulfur below 0.01 percent on some specs), and certify hardness on the MTR. On the PO, the correct phrasin' is: “ASTM A105 per NACE MR0175 / ISO 15156-2, 187 HBW max, normalized, MTR with hardness required.” Anything more vague and the compliance chain got gaps in terms of material provided, since often times A105 is just used as structural steel.
Alloy and CRA Flanges: A182 and the Part 3 Rules
ASTM A182 alloy flanges (F5, F9, F11, F22, F91) and stainless and CRA flanges (F304L, F316L, F22, F51 duplex, F55 super duplex, F60 lean duplex) all got specific requirements in MR0175 Part 2 or Part 3 dependin' on chemistry. 22Cr duplex (F51) and 25Cr super duplex (F55) are common upgrades for more aggressive sour service, but dey come with specific PREN (Pitting Resistance Equivalent Number) targets and mandatory solution annealing. Hardness ceilings apply across the board. For 316L specifically, there's a partial pressure limit above which it ain't acceptable no matter the hardness, so “stainless is always fine for sour” ain't a correct assumption, y’all. When in doubt, check the relevant MR0175 annex table against your actual H2S partial pressure, pH, and temperature.
Bolting: B7M, L7M, 2HM, and Why Standard B7 Won’t Fly
Dis is where a whole lot of otherwise clean sour service jobs come apart. Standard ASTM A193 B7 studs, the default bolting for nearly every flanged joint in industry, ain't acceptable for NACE MR0175 service. The B7 hardness ceiling is 35 HRC. The sour service ceiling for the same chemistry in the B7M variant is 22 HRC. Same steel, different temperin', different hardness, different compliance status. What y'all actually need on a sour joint:
ASTM A193 B7M studs for standard sour carbon steel bolting. ASTM A320 L7M studs for low-temperature sour service where Charpy impact is also required. ASTM A194 Grade 2HM heavy hex nuts (22 HRC max, matched to B7M). ASTM A194 Grade 7M nuts for the lower temperature cases. B7M and 2HM cost more than B7 and 2H and often carry longer lead times. A common procurement mistake is specifyin' the right flange and forgettin' the bolting, which takes the whole joint out of compliance.
Gaskets, Face Prep, and the Things Folks Forget
Ring Type Joint (RTJ) rings made from soft iron, low carbon steel, or a NACE-compliant CRA are the default for sour service at higher pressure classes. Spiral wound gaskets with 316L windings may need a nickel-based or CRA filler dependin' on H2S exposure. The face prep notes in MR0175 apply too: no hard machinin' residues, no surface contamination. The carbon steel weld filler metal for the weld neck has to be compatible. And the MTR for every component needs to trace back to the heat number. None of dis is optional, and all of it is a line item on a real sour service PO.
What to Actually Ask For on the RFQ
When a sour service RFQ goes out, the clean version reads like dis:
Quantity, size, class, facing, and type. Material: “ASTM A105 per NACE MR0175 / ISO 15156-2, 187 HBW max, normalized.” MTR: “Required with heat number, chemistry, mechanical properties, and hardness.” Bolting: “ASTM A193 B7M studs, ASTM A194 2HM heavy hex nuts, per NACE MR0175.” Gasket: “RTJ octagonal soft iron” or “spiral wound with CRA filler,” NACE compliant. Documentation: “CofC referencing NACE MR0175 / ISO 15156, heat number traceable.”
Dat RFQ locks every component to the same standard from day one and keeps the shop from havin' to call you back for clarifications.
Closin' the Loop
NACE MR0175 ain't optional on a sour service job, and it ain't somethin' y'all want to sort out after the PO's already been cut. Get the flange material, the bolting, and the gasket lined up to the same standard up front. If you got a sour service bid package and want to confirm what’s compliant, line up lead times on B7M and 2HM combos, or pin down the MTR requirements before quotin', holler at Texas Flange. For related readin', our deep dive on RTJ flanges covers ring gasket specification for sour and API 6A service in detail.
Texas Flange & Fitting Supply | 281-484-8325 | texasflange.com