By Texas Flange TeamUncategorized
In the industrial world, I tell you what, a “close enough” measurement is mighty often the recipe for a leak, a stripped thread, or a costly shutdown. Whether y'all are puttin' together a high-pressure pipeline in a refinery or fixin' a lightweight aluminum flange for a fluid treatment facility, the integrity of your connection rides entirely on the fasteners holdin' it together.
Now, accurate bolt dimensions (specifically diameter, thread pitch, and length) are the foundation of reliable mechanical fastenin' and leak-free flange assemblies. If you’ve ever stood in a warehouse holdin' a greasy bolt, tryin' to figure out if it’s an M12 or a 1/2-inch UNC, well, you know it ain't always as easy as passin' the eye test.
This guide goes past the basics to hand y'all some practical tips, clears up the mighty confusin' mix of metric and imperial standards, and explains how gettin' your sizing right directly touches safety. We'll cover how to spot major, minor, and shank diameters. We'll also talk about how to work a thread pitch gauge right, and the specific rules for measurin' bolt length across different head types.
Finally, we'll look at why all dis matters for Texas Flange customers, specifically when it comes to ASME flange stud bolts and flange bolt kits. Dat'll help y'all turn raw measurements into the right fastener choices for your next job.
How Do Y'all Measure Bolt Diameter Right?
When somebody asks for the “size” of a bolt, dey're almost always talkin' about the nominal diameter. Dat's the major diameter of the threaded part, from one outside edge clean across to the other. Gettin' dis number right is the first step to correct hole sizin', proper thread engagement, and a clamp load you can count on under torque.
Now if the diameter is off, the bolt might feel loose in a tapped hole (strippin' risk) or just plain won’t fit through the clearance hole of a flange. Y'all should always give a bolt a good lookin'-over to see if the threads got damaged before you install it.
The Three Critical Diameter Measurements
To really understand a fastener like a bolt, you gotta look at it in three dimensions. Knowin' dese dimensions helps when you're orderin' replacements or designin' a joint dat needs a specific shear strength.
-
Major Diameter (The Nominal Size): Dis is the largest diameter measured across the crests (the very tops) of the threads. If you measure a bolt and it reads 0.498 inches, it's likely a nominal 0.500-inch (1/2-inch) bolt. Manufacturers always make bolts a hair under the nominal size so dey'll fit into the mating nut or tapped hole, since an oversize thread just won’t fit.
-
Minor Diameter (The Root): Dis is the smallest diameter, measured at the root (the bottom/valley) of the thread groove. Y'all won’t use dis number much to reference bolts, but engineers use it to figure the “tensile stress area” – essentially, how much metal is really dere to hold the load before the bolt snaps.
-
Shank Diameter (The Body): Dis is the smooth, unthreaded part of the bolt shaft, assumin' the bolt ain’t fully threaded. In a lot of heavy-duty flange connections, the shank diameter gives you the bearin' surface. For high-precision fitments, the shank is often ground to a specific tolerance to match the engineerin' requirements.
The Technician’s Measurement Checklist
Before y'all start measurin', here's a practical workflow to help you dodge as many false readin's as possible:
-
Zero the Tool: If you're usin' digital calipers, make sure dey're calibrated. Close the jaws all the way and hit the “Zero” button. A speck of dirt or metal on the jaw can throw your measurement off by 0.05 mm, so calibration matters, friend.
-
Check for Burrs: If the bolt has been used, check the threads for dings or burrs. Measurin' over a damaged thread'll give you a bigger diameter than what's really dere.
-
Measure the Shank for Roundness: Move your caliper jaws to the unthreaded shaft. Take a measurement, rotate the bolt 90 degrees, and measure again. Dis helps y'all spot “ovality,” where a bolt got warped or stretched out of round.
-
Go Across the Crests: For the major diameter, set the broad, flat part of the caliper jaws across the threads. Don't use the sharp tips of the jaws, 'cause dey can slip into the thread grooves and give you a bad readin'.
Which Tools Work Best for Measurin' Bolt Diameter?
Y'all don’t need a laboratory to measure bolts, but you do need the right tools for the job. For example, usin' a tape measure to figure if a bolt is 9/16″ or 5/8″ is a gamble you shouldn’t take, though it could be handy for overall length. Here's how dese tools stack up:
1. Digital Calipers
For 95% of field work, a good set of digital calipers is the gold standard. Dey give you a mighty fine balance of speed and accuracy, typically readin' down to 0.01 mm or 0.0005 inches. Dey're versatile enough to measure several dimensions on a part, includin' the outside diameter, inside diameter, and depth / overall length.
2. Micrometers
If you're workin' with critical machined shafts or need to check the shank diameter for a tight tolerance bearin' fit, grab yourself a micrometer. Micrometers ain’t convenient for threads, but dey can give you more practical precision on smoother surfaces.
3. Optical Comparators & CMMs
Y'all won’t use dese in the field, but in manufacturin' plants, dese tools use light or touch probes to map the exact geometry of a thread profile. Dat's how manufacturers prove a batch of ANSI flange stud bolts meets the strict ASME B16 standards before dey ship out to you.
4. Bolt Gauges / Thread Detective
Dese are the plastic or metal templates y'all often see hangin' in hardware stores. Dey're mighty good for a “quick check” to separate your metric stock from your imperial stock, but don't y'all use 'em for critical engineerin' verification.
What Is Bolt Thread Pitch and How Is It Measured?
Once y'all know the diameter, you've covered the most important measurement. But you need the thread pitch too. Dat's where most installation errors happen. For instance, a 1/2-inch bolt can come in both Coarse (13 threads per inch) and Fine (20 threads per inch). Try to mix 'em and you'll cross-thread the fastener, ruinin' both the bolt and the nut.
Metric vs. Imperial: Two Different Languages
The world's split into two systems, and dey measure pitch different:
-
Imperial (US Customary): Uses TPI (Threads Per Inch). You're literally countin' how many thread peaks sit within one inch of length.
-
Example: 1/2″-13 means a half-inch diameter with 13 threads per inch.
-
Metric (ISO): Uses Pitch. Dis measures the actual distance between one thread crest and the next in millimeters.
-
Example: M12 x 1.75 means a 12mm diameter where the distance between each thread is 1.75mm.
Crucial Note: A higher number in Imperial means a finer thread (more threads packed into an inch). A higher number in Metric means a coarser thread (a wider distance between threads). Don't get it backwards, now.
How to Use a Thread Pitch Gauge
The most reliable way to identify pitch is workin' a thread pitch gauge. Dat gauge looks like a Swiss Army knife with serrated metal leaves.
-
Pick a leaf dat looks close to your bolt‘s threads.
-
Press the teeth into the threads of the bolt.
-
Check for light: Hold it up to a light source. If you see gaps between the gauge and the bolt, it ain’t a match. The gauge oughta fit snug like a puzzle piece.
-
Read the stamp: The leaf'll be stamped with the size in metric or imperial.
Reference Table: Common Thread Standards
|
Thread Standard
|
Pitch / TPI
|
Typical Application
|
|---|---|---|
|
UNC (Unified National Coarse)
|
8–16 TPI (Typical)
|
The standard for general construction and industrial flanges. Coarse threads go together faster and put up with dirt and damage better.
|
|
UNF (Unified National Fine)
|
16–32 TPI (Typical)
|
Used in automotive or aerospace work where higher tensile strength and finer tension adjustment are required.
|
|
ISO Metric Coarse
|
1.0–2.5 mm
|
The global standard for general engineerin'. Most “standard” metric bolts are coarse pitch.
|
|
ISO Metric Fine
|
0.75–1.5 mm
|
Used for precision assemblies and thin-walled components.
|
How Is Bolt Length Measured? (It’s Not Always End-to-End)
Dis is maybe the most common mistake folks make when orderin' replacement flange bolt kits. If you measure the bolt wrong, you might end up with a bolt dat bottoms out in a blind hole or one dat doesn’t leave enough thread stickin' out for the nut to grip safe. The rule of thumb depends entirely on the Head Style:
1. Hex Bolts, Flange Bolts, and Socket Head Cap Screws
For any bolt where the head sits on top of the surface, you measure the length from underneath the head to the tip of the bolt.
-
Why? 'Cause the head ain't part of the material thickness bein' fastened. The length is the part of the bolt dat goes into the assembly.
2. Flat Head / Countersunk Bolts
For bolts built to sit flush with the surface (like in a countersunk hole), you measure the length from the very top of the head to the tip.
-
Why? 'Cause the head actually takes up space inside the hole. The whole fastener length is part of the fitment.
3. Stud Bolts (for Flanges)
In the world of industrial flanges (like the ones Texas Flangesupplies), we mostly use stud bolts—threaded rods with nuts on both ends.
-
Measurement: Studs get measured from first thread to first thread (leavin' out the chamfered points at the ends). But always check if your spec calls for “Overall Length” (OAL), which may or may not include the tip dependin' on the inquiry.
-
Pro Tip: When in doubt, give your supplier the “Effective Thread Length”.
Metric vs. Imperial: The Conversion Headache
“Can I just use an M8 bolt in a 5/16 hole?”
The short answer: No.
While 8mm (0.315″) and 5/16″ (0.3125″) are mighty close in diameter, the thread pitches will almost never line up right. Forcin' a metric bolt into an imperial nut might work for the first two turns, but it'll bind up eventually. If you force it with a wrench, you're just cuttin' new threads and wreckin' the integrity of the connection.
When to Convert and When to Replace
If you're runnin' a facility with legacy equipment, y'all likely got a mix of ASME (Imperial) and ISO (Metric) equipment.
-
Best Practice: Keep separate bins. Never mix stocks, now.
-
Emergency Fixes: If you absolutely gotta convert a hole from one standard to another, the safe way is to drill and re-tap the hole to the new size, or use a thread insert (Helicoil). Don't y'all lean on “close enough” thread engagement.
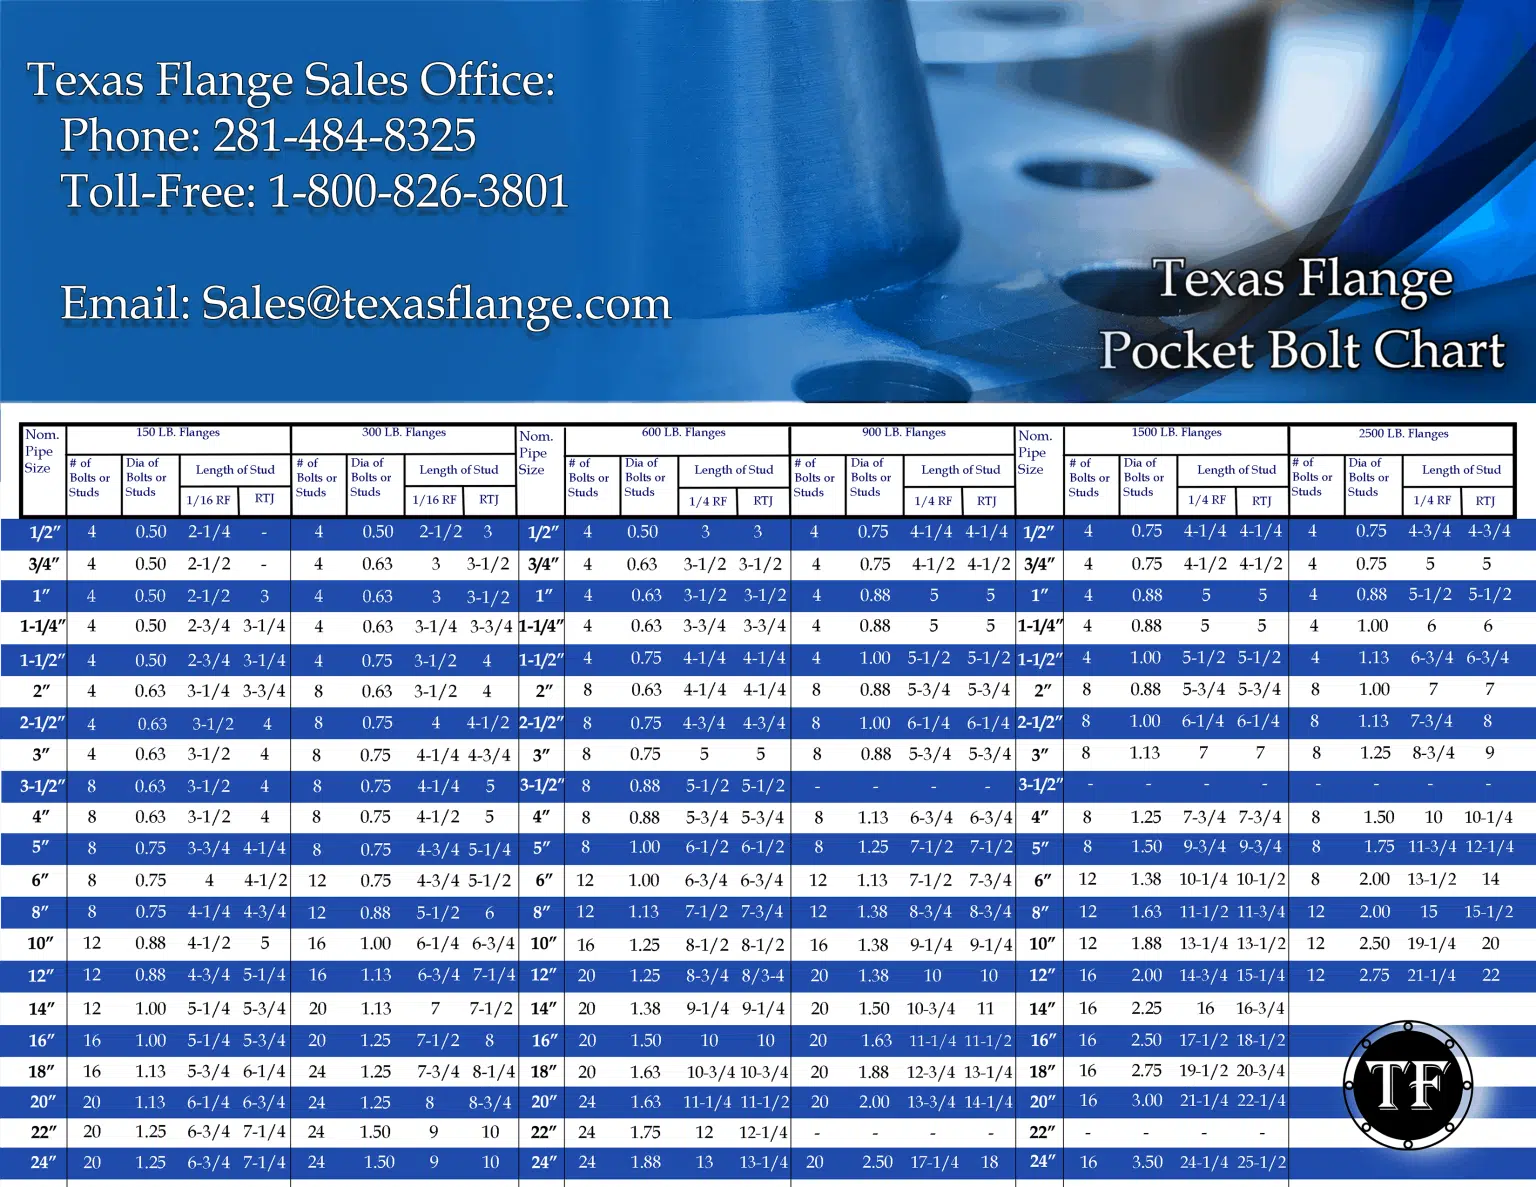
A handy tool for the office is a bolt diameter chart dat lists both decimal equivalents and thread pitches side-by-side. Dat keeps y'all from guessin' whether dat rusty bolt on the workbench is an M12 or a 1/2″. Y'all can check our ASME B16.5 flange bolt chart for recommended dimensions for ASME flange hardware.
Why Bolt Dimensions Are Critical for Flange Assemblies
Here at Texas Flange, we see the results of improper bolting ever' day. In a flange assembly, the bolt acts like a spring. You stretch it (by torquin' the nut), and its want to snap back is what makes the clamp load dat crushes the gasket and seals the pipe connection.
The Aluminum Flange Factor
If you're workin' with aluminum flanges (a growin' interest for lightweight industrial jobs), precision matters even more.
-
Soft Material: Aluminum is softer than carbon steel. If you use a bolt with the wrong length and it bottoms out, you might strip them aluminum threads instantly. Torque values will vary.
-
Load Distribution: 'Cause aluminum flanges can flex more than steel, you gotta make sure you're usin' the right number of bolts and dat dey're spaced right (the Bolt Circle).
-
Galvanic Corrosion: If you use standard stainless steel bolts on an aluminum flange, you've made yourself a battery. Dat aluminum could corrode fast. You gotta measure for and install insulatin' washers or sleeves, which changes the bolt length you need.
ASME B16.5 Standards
For most industrial work, y'all ain’t guessin' at the dimensions; you're followin' a map. The ASME B16.5 standard lays out the bolt circle, number of bolts, and diameter for every pressure class (150#, 300#, etc…). The ASME B16.5 flange bolt chart lists the count, diameter and stud length for every size.
-
Example: A 4-inch Class 150 flange will always need eight 5/8-inch diameter bolts, unless you change the bolt pattern for a custom job. See the Class 150 bolt circle dimensions.
-
Knowin' dese standards helps y'all order pre-packaged ASME flange stud bolts without havin' to measure every last existin' bolt on a corroded pipe. With the size confirmed, check bolt torque by pressure class.
Summary: How to Make Sure Y'all Order the Right Fasteners
Measurements are only as good as what you do with 'em. Whether you're maintainin' a refinery in Texas or buildin' a custom skid, follow dis updated checklist to make sure y'all get the right hardware:
-
Check the Head Style: Are you measurin' under the head (Hex) or overall (Countersunk)?
-
Verify the Diameter: Use calipers to get the Major Diameter, then round to the nearest nominal size.
-
Confirm the Pitch: Use a pitch gauge. Don't guess, now. Is the thread coarse or fine?
-
Check the Grade: Dimensions aren’t everything. A Grade 8 bolt has different strength properties than a Grade 5, even if dey measure the same.
-
Consult the Standard: If the work's bein' done on flanges, look at the ASME B16.5 tables. It's safer to check first based on the flange size and class than to measure a potentially wrong bolt currently installed in the field.
Need Help with Flange Fasteners?
If y'all are lookin' for reliable flange bolt kits, custom studs, or aluminum flange solutions, accuracy is our business. Don’t risk downtime with hardware dat don't match.
Contact Texas Flange today to talk about your project requirements. Our crew can help y'all find your way around the charts, check your dimensions, and point you the right direction so you get the exact hardware you need for a safe, leak-free connection.
Key Takeaways for the Technician
-
Diameter: Measure the crests for the major diameter.
-
Pitch: Use a gauge to tell Metric (mm) from Imperial (TPI).
-
Length: Under the head for hex, or top of the head for countersunk.
-
Safety: Never force mismatched threads. Replace with the exact standard.
By masterin' these simple measurements, you protect your equipment, your people, and your project timeline. Dat's how we do it down on the bayou.